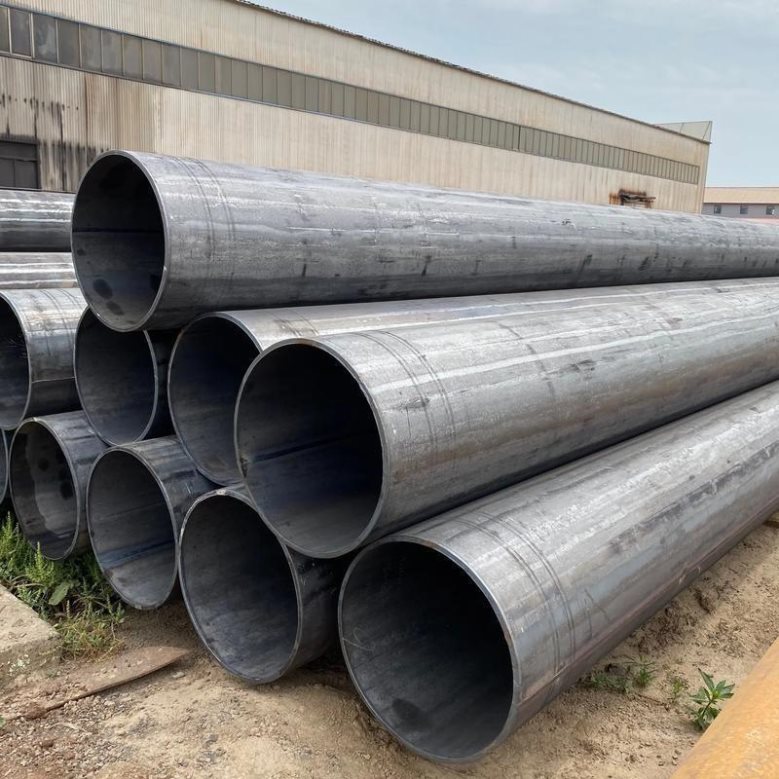


Carbon Steel LSAW Pipe
Products Description
|
Diameter |
406mm- 1118mm (16 "- 44") |
|
Thickness |
6.0-25.4mm 1/4 "-1" |
|
Standard |
API,DNV,ISO,DEP,EN,ASTM,DIN,BS,JIS,GB,CSA |
|
Length |
5.8m,6m,12m,18m, ect. |
|
Steel Grade |
API 5L A- X70. |
The Comparison between Carbon Steel LSAW pipe and SSAW Pipes
|
Comparison Dimension |
LSAW (Longitudinal Submerged Arc Welded Pipe) |
SSAW (Spiral Submerged Arc Welded Pipe) |
|
Full Name |
Longitudinal Submerged Arc Welded Pipe |
Spiral Submerged Arc Welded Pipe |
|
Raw Material |
Single thick steel plate (thickness up to 50mm or more) |
Hot-rolled steel strip (narrower width, flexible adjustment) |
|
Forming Process |
Plate pre-bent and formed via JCO/UOE method; seam runs parallel to pipe axis |
Strip continuously spirally wound at an angle (typically 10°-30°); seam follows a helical path |
|
Welding Method |
Double-sided SAW, often with four-wire tandem welding; longitudinal straight seam |
Double-sided SAW; continuous helical seam, 30%-100% longer than straight seam of equivalent length |
|
Typical Diameter Range |
Ф406.4mm - Ф1422.4mm |
Ф 219 mm - Ф 2540mm |
|
Typical Wall Thickness Range |
8 mm - 50mm |
6mm - 25mm (standard), up to 30mm with specialized processes |
|
Pressure Rating |
High pressure (≥10 MPa); suitable for X70-X120 high-grade steels; meets Class 1-2 area safety requirements |
Medium to low pressure (typically ≤10 MPa); suitable for X60-X80 grades; commonly used in Class 3-4 areas |
|
Geometric Accuracy |
High (ovality ≤0.5%D, straightness ≤1.5 mm/m); stable dimensions after expansion |
Lower; weld cap control critical (≤2.5 mm); prone to "saddle" or "fishback" internal weld profiles |
|
Residual Stress |
Uniformly distributed; largely eliminated by hydraulic expansion |
Complex and uneven; predominantly tensile state |
|
Weld Strength Characteristics |
Shorter weld, fewer defects, lower stress concentration; higher burst pressure than SSAW |
Helical seam disperses primary stress; superior crack arrest performance; failure confined to single pitch |
|
Static Burst Strength |
Higher yield and burst pressures; optimal for high-pressure, high-stress environments |
Slightly lower burst pressure; superior ductility and crack propagation resistance |
|
Primary Production Standards |
API 5L, GB/T 9711, ASTM A671, ISO 3183 |
API 5L, GB/T 9711, ASTM A671, ISO 3183 |
|
Equipment Investment |
High (requires large JCO/UOE presses, expansion machines) |
Lower (simpler coiling equipment, reduced infrastructure cost) |
|
Production Efficiency |
Lower (single-plate processing, complex) |
Higher (continuous strip feeding, ideal for high-volume production) |
|
Typical Application Fields |
Mainline oil/gas pipelines, subsea pipelines, arctic regions, urban dense zones, deepwater projects, high-pressure systems |
Long-distance pipelines (non-high-pressure sections), water transmission, municipal networks, heating lines |
|
Coating Compatibility |
Fully compatible with 3PE, FBE, IPN8710; strong adhesion |
Compatible with major coating systems; weld cap may affect uniformity, requiring special treatment |
|
Typical Project Examples |
West-East Gas Pipeline (X70, Φ1016 mm), Nord Stream, Gulf of Mexico deepwater pipelines |
West-East Gas Pipeline Line IV (Φ1219 mm, X70), Guliang-Hekou connecting line (18 m ultra-long pipes), urban water networks |
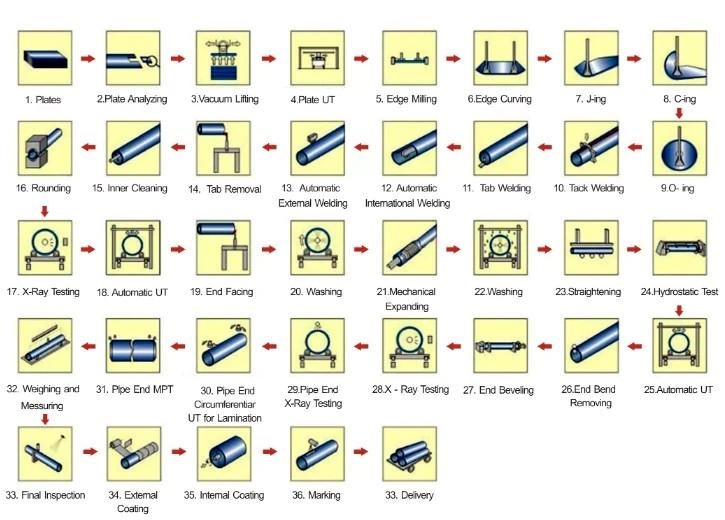
Production Process of Carbon Steel LSAW Pipe
The inspection before Seam Welding
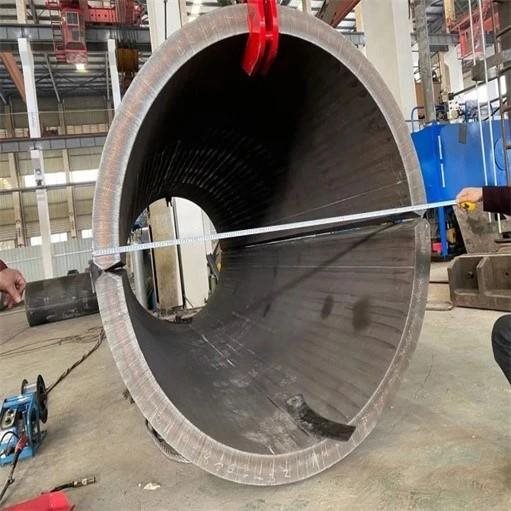
Diameter Inspection
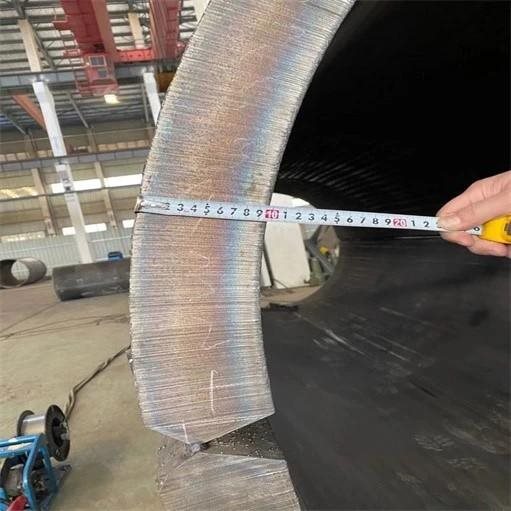
Thickness Inspection
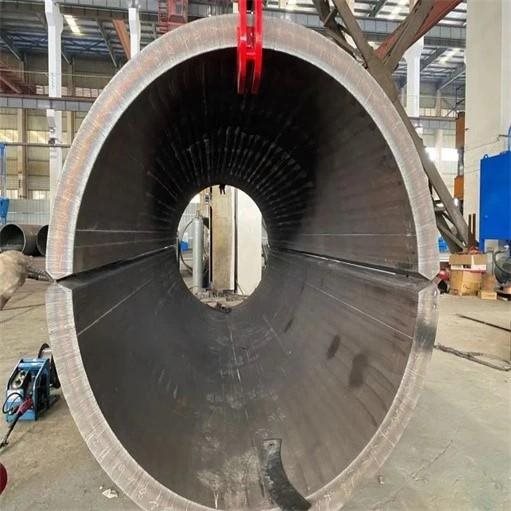
Finished Inspection
Inspection after Production
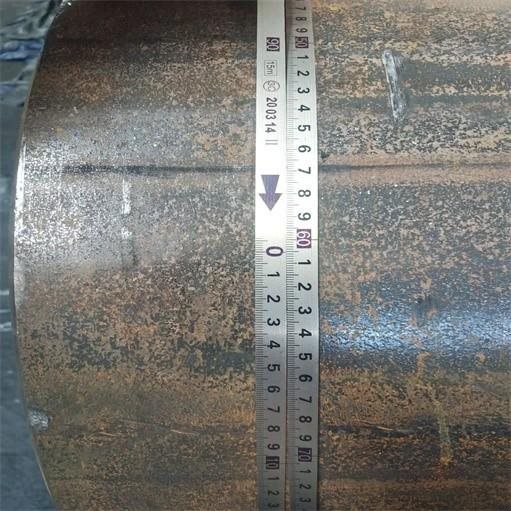
Diameter Inspection
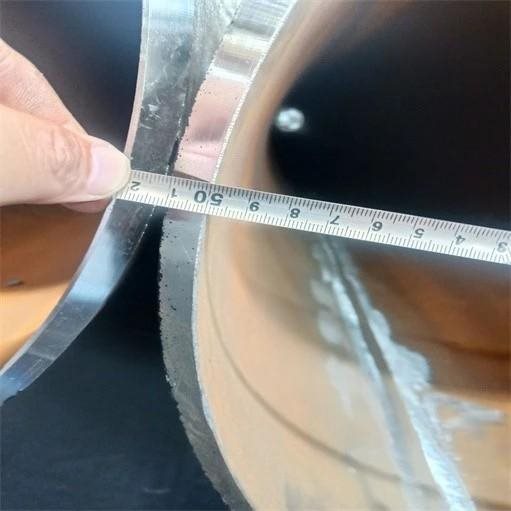
Diameter Inspection
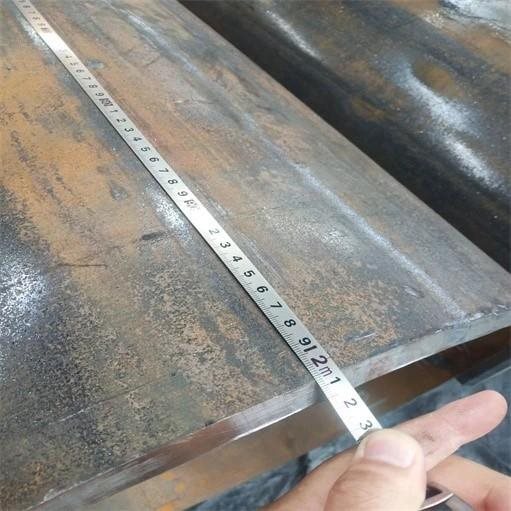
Length Inspection
Product Show